Essential details
Shipping:Ocean freight
Product Introduction
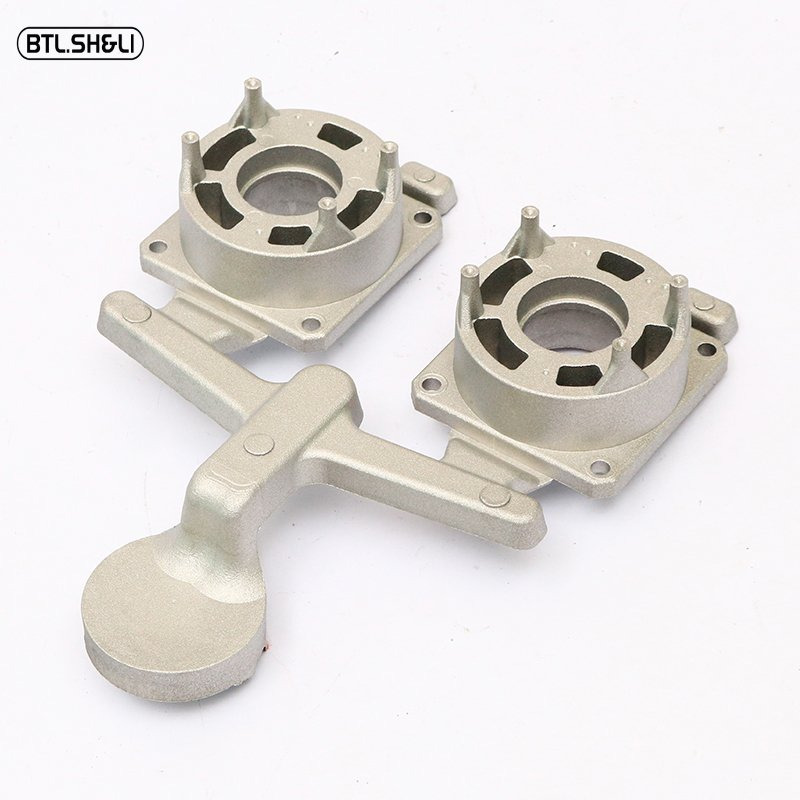
Motor end caps produced in a two-cavity die. The bearing seat and locating step are formed in the same casting, so once fitted to the housing the rotor stays concentric. Mounting holes around the rim line up with the housing threads, removing the need to match-drill at assembly, and the two-cavity tool keeps left and right caps dimensionally identical. They suit small motors, pumps and geared motors, with frame size and bearing number adapted to your design. Bearing bores are machined after casting to the required fit. The two cavities produce left and right caps, machined in the same batch so rotor concentricity stays stable after assembly.
